How to Verify Screw Compressor Vibration Data
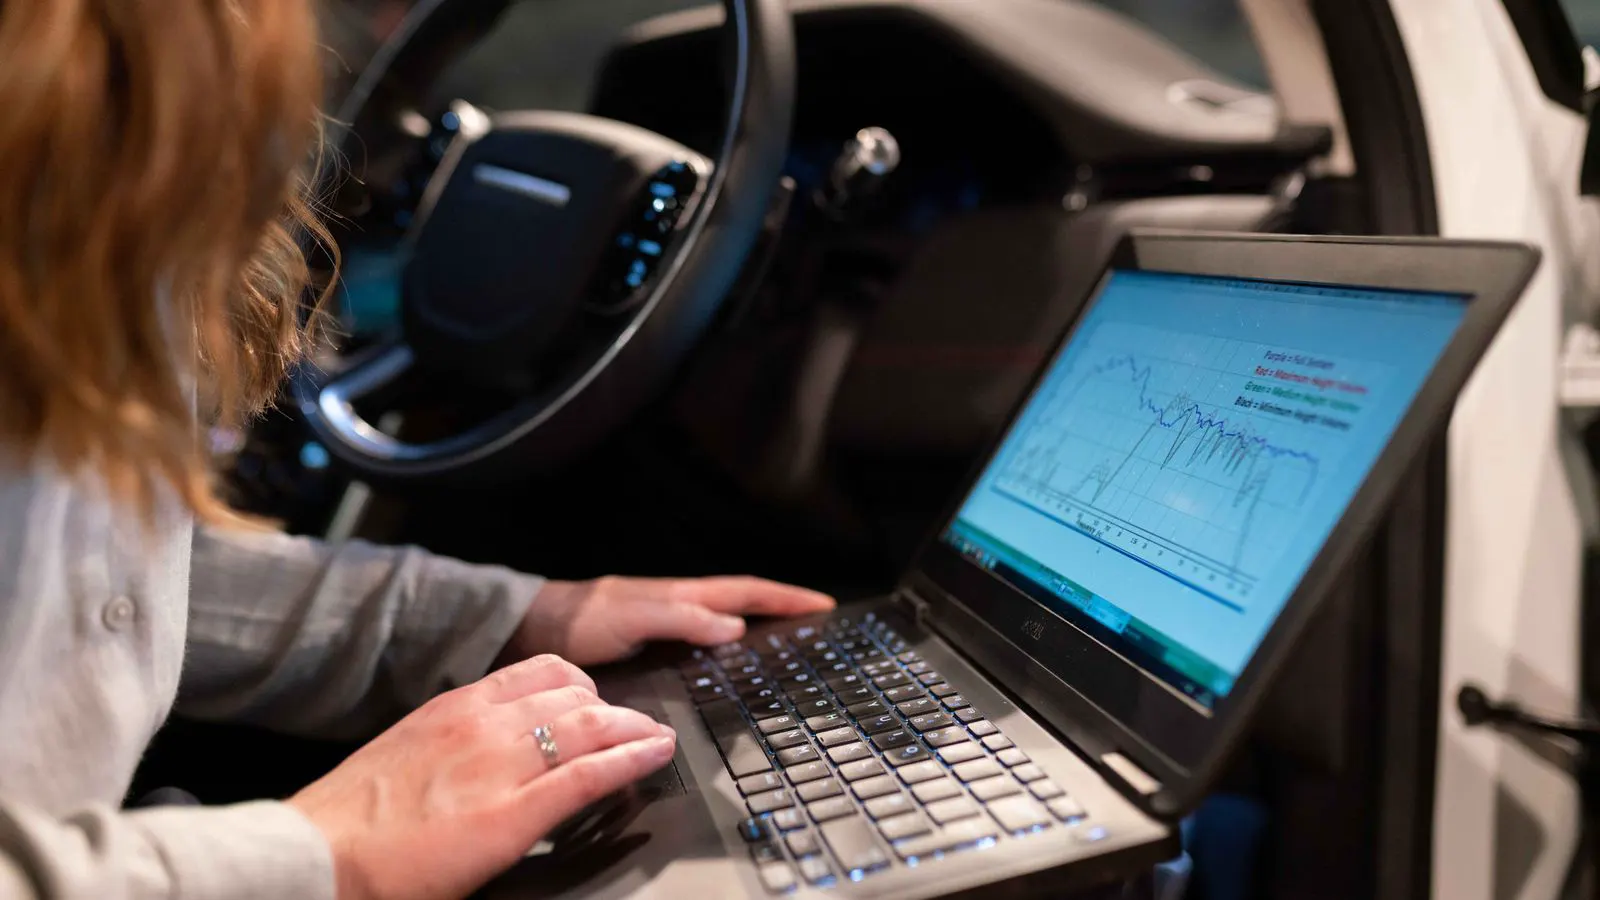
Verify screw compressor vibration by mounting calibrated accelerometers on the frame and drive units, recording time-domain and frequency data, and comparing results against ISO 10816 severity zones. This confirms rotor alignment, bearing condition, and coupling integrity before failure occurs.
- Use calibrated accelerometers and record both time-domain and frequency-domain data
- Compare measured values against ISO 10816 severity zones for context
- Check mounting torque, sensor orientation, and cable strain before reading results
- Correlate vibration patterns with operating speed to identify shaft misalignment or imbalance
- Maintain a baseline dataset for comparison during routine inspections
Why vibration data matters for screw compressors
Screw compressors operate under high rotational loads and continuous duty cycles. The rotor assembly, bearings, and coupling all transmit forces into the machine frame. When any of these components wear or shift, those forces change in frequency, amplitude, or both.
Vibration testing gives you a measurable record of those changes. A single reading is not enough. You need a baseline, a trend, and a clear interpretation against recognized thresholds. This article walks through the practical steps to collect and verify that data.
What you need before starting
Do not skip preparation. Vibration readings are only as good as the setup that produced them.
- A calibrated piezoelectric or MEMS accelerometer suitable for the frequency range of your compressor (typically 10 Hz to 10 kHz for most industrial units)
- A data acquisition system or portable recorder capable of capturing time-domain waveforms and computing spectra
- Magnetic or stud mount with appropriate coupling medium
- A torque wrench for stud mounts, if used
- A reference to ISO 10816 or ISO 10821 for severity classification
- The compressor nameplate data: rated speed, service hours, and last major maintenance date
- A clean, accessible mounting surface free of loose fasteners or paint buildup
Step 1: Inspect the mounting surface
Remove loose bolts, scale, or paint from the area where the sensor will attach. The goal is a rigid, direct path from the machine structure to the sensor diaphragm.
If the surface is soft or coated with a thick layer of paint, the sensor will not capture the true structural vibration. It will filter out high-frequency content and produce values that look lower than reality.
Reason: Accurate vibration measurement requires a solid mechanical connection between the structure and the sensor.
Step 2: Choose the correct sensor orientation
Mount the accelerometer with its sensitive axis perpendicular to the direction of the expected vibration. For screw compressors, the most diagnostic directions are usually vertical (up-down), horizontal (side-to-side), and axial (along the shaft).
If your compressor has a horizontal shaft, axial vibration is particularly useful for detecting coupling and bearing issues. Vertical vibration often indicates rotor imbalance or structural looseness.
Reason: Vibration is a vector quantity. Measuring the wrong axis gives you a partial picture and can mask a real problem.
Step 3: Secure the sensor with the correct mounting method
Magnetic mounts are acceptable for quick field checks and for frequencies above roughly 50 Hz. For sustained monitoring or detailed diagnostics, use a stud mount with a thread lock or a stud with a thin layer of grease or epoxy.
Tighten the stud to the manufacturer’s torque specification. Check the torque after the first operating cycle. Thermal cycling can loosen fasteners.
Reason: Loose or improperly coupled sensors add noise to the signal and reduce the reliability of frequency analysis.
Step 4: Record a baseline at rated speed
Bring the compressor to its normal operating speed. Let it stabilize for at least five minutes. Record data for a minimum of sixty seconds at each of the three axes.
Capture both the time-domain waveform and the frequency spectrum. The time record shows shock events and transient spikes. The spectrum shows which frequencies dominate and whether they align with shaft frequency, bearing defect frequencies, or structural resonances.
Reason: A baseline at rated speed gives you a reference for comparison. Without it, a single reading has little diagnostic value.
Step 5: Run a speed ramp if available
If your compressor control allows a slow ramp from low to rated speed, record vibration at several intermediate speeds. This helps separate problems caused by imbalance from problems caused by misalignment.
Imbalance tends to produce vibration that grows with the square of speed. Misalignment produces vibration that grows linearly with speed and often appears at twice the shaft frequency.
Reason: Speed-ramp data reveals the relationship between rotational speed and vibration amplitude, which is the key to identifying the root cause.
Step 6: Compare measured values against ISO 10816 severity zones
ISO 10816 classifies vibration levels into four severity zones based on RMS values in mm/s:
| Severity Zone | Description | Typical Action |
|---|---|---|
| Zone 1 | Acceptable | Normal operation, no immediate action |
| Zone 2 | Acceptable | Monitor, no corrective action required |
| Zone 3 | Unacceptable | Investigate source, schedule maintenance |
| Zone 4 | Dangerous | Stop operation, immediate inspection |
The specific threshold values in mm/s depend on machine class, speed, and service conditions. ISO 10816 provides charts for different speed ranges. Use the chart that matches your compressor’s rated speed.
Reason: Severity zones give you a standardized, defensible way to classify what the numbers mean in operational terms.
Step 7: Analyze the frequency spectrum for characteristic patterns
Look for peaks that match known fault signatures:
- Shaft frequency peaks: Often indicate imbalance or loose mechanical parts
- 2x shaft frequency peaks: Common with misalignment or bent shafts
- Bearing defect frequencies: Appear as discrete peaks at specific harmonic relationships to shaft speed; these indicate rolling element or cage wear
- High-frequency broadband energy: Can indicate cavitation, loose components, or structural resonance
If the spectrum is dominated by a single frequency at 1x shaft speed, the issue is more likely imbalance. If you see strong 2x content alongside 1x, check coupling and alignment. If you see multiple discrete peaks at non-integer harmonics, inspect the bearings.
Reason: Frequency analysis separates the “what” from the “why.” RMS values tell you severity; the spectrum tells you the likely mechanical cause.
Step 8: Verify the data against operating conditions
Before drawing conclusions, confirm that the compressor was running under normal conditions. Check the pressure gauge, the oil pressure (if applicable), and the motor current draw.
A compressor operating at low load, with a partially blocked discharge line, or with an open bypass will show lower vibration than one at full rated load. Conversely, an over-pressurized or unstable discharge condition will increase vibration.
Reason: Vibration is a function of load as well as mechanical condition. A reading taken under abnormal operating conditions can be misleading.
Step 9: Document and archive the results
Record the date, operator, sensor serial number, calibration date, mounting location, orientation, speed, load, and ambient conditions. Save the raw waveform files and the processed spectra.
Keep these records in a maintenance log or a CMMS. The value of vibration data increases over time as you build a trend. A machine that was in Zone 2 for six months and is now in Zone 3 has a different story than a machine that was already in Zone 3 and is now in Zone 4.
Reason: Trend analysis is more reliable than single-point measurements. It catches slow degradation before it becomes a failure.
Common mistakes that invalidate the data
- Using a magnetic mount on a soft surface. The magnet adds a mass-spring system that filters out high frequencies. Use stud mounts for anything below 50 Hz or for detailed bearing diagnostics.
- Recording at a speed different from rated speed. Compare like with like. A reading at 85% speed is not directly comparable to a reading at 100% speed.
- Ignoring sensor calibration. A sensor that drifted out of calibration by 10% can push a borderline reading into a different severity zone.
- Not checking cable strain. A kinked or pinched cable can introduce noise or break the signal intermittently.
- Assuming low vibration means healthy. A badly worn bearing can sometimes produce low RMS values if the wear pattern is not exciting the structure strongly. Always check the spectrum, not just the RMS number.
Final verification: repeat the measurement
After completing the full sequence, repeat the measurement at the same location and orientation. If the readings differ by more than 10% from the first pass, stop and check the mounting, the sensor, and the data acquisition system before proceeding.
A consistent repeat is your confidence check. If the first pass shows Zone 3 vibration at 2x shaft frequency and the second pass shows the same, you have a reliable data point. If the second pass shows Zone 2, something in your setup changed, and you should not trust either reading until you identify why.
This final step protects you from false alarms and missed faults. It also gives you a defensible record: two independent measurements that agree, taken by the same method, on the same day, at the same operating point.
Frequently asked questions
How often should I record vibration data on a screw compressor?
Record a baseline at commissioning, after any major repair, and then at regular intervals such as quarterly or semi-annually. Increase frequency if the machine shows early signs of wear or if it runs in a critical process.
Can I use a smartphone app for vibration testing on a screw compressor?
Smartphone apps can provide a rough indication of vibration levels for quick checks, but they lack the calibrated sensors, frequency resolution, and data quality needed for diagnostic work. Use dedicated equipment for any decision that affects maintenance or safety.
What vibration level is too high for a screw compressor?
There is no single universal limit. ISO 10816 defines severity zones that depend on machine speed and class. A value that is acceptable for a low-speed machine may be dangerous for a high-speed unit. Always use the correct chart for your specific compressor.
Do I need to measure all three axes, or is one enough?
One axis is not enough for a full diagnostic. Vertical, horizontal, and axial measurements each reveal different fault patterns. Axial vibration is especially useful for catching bearing and coupling issues that vertical and horizontal readings can miss.
What if the vibration is in Zone 3 but the compressor still runs fine?
Zone 3 means the vibration is above the threshold for normal operation and indicates a condition that will likely worsen. The machine may continue to run for a time, but the risk of accelerated wear or sudden failure increases. Schedule an inspection and re-test after correction.